Weld Fasteners
Weld nuts that fuse into sheet-metal assemblies — square per DIN 928 and hex per DIN 929 — replacing tapped holes where the far side of the panel is unreachable.
Weld nuts against tapped holes and through-bolting
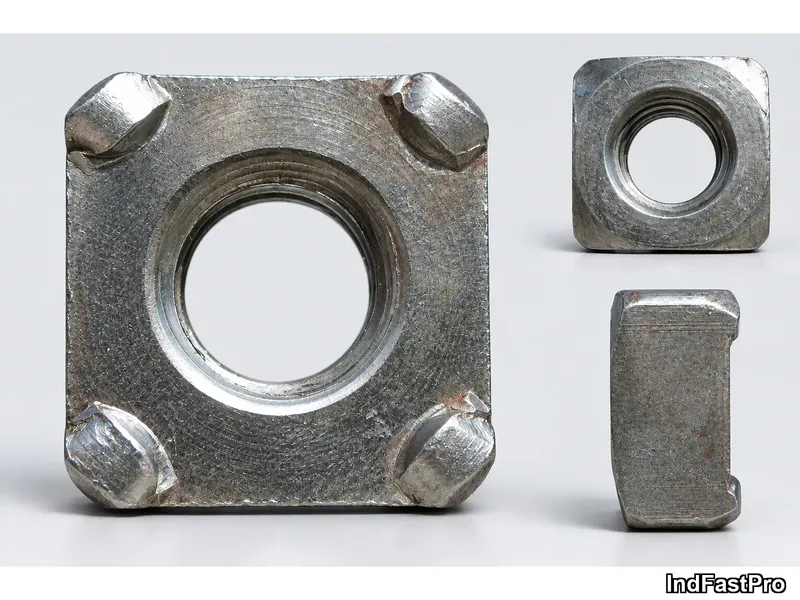
Weld nuts per DIN 928 (square, with projections) and DIN 929 (hex, welded face) earn their place in an assembly wherever the far side of a sheet joint is unreachable or a tapped hole would leave too little material. The projections fuse into the sheet under electrode pressure, so the decisions that matter are sheet thickness and weldability of the base material, electrode access on the projection side, and the coating interaction — pre-plated sheets change the welding window, and the weld parameters must be verified on the actual sheet lot, not on bare coupons. Where the sheet is galvanized or pre-coated, we quote the weld trial expectation together with the nut, because that trial decides the process as much as the fastener does.
Against the alternatives, the choice is concrete: a drilled-and-tapped stud or hole preserves disassembly but consumes sheet thickness and machining time on the far side; through-bolting with a nut avoids welding entirely but needs access to both faces and a clamping path through the whole stack; a weld nut needs single-side access only and survives the life of the assembly as a permanent threaded location. Corrosion at the weld line, thread protection during welding (a gauge or bolt protects the thread through the thermal cycle) and the inspection method for weld quality are the practical boundary conditions. Tell us the sheet material and thickness, the weld equipment available, and the service environment, and we will propose the nut form, weld spec expectation and thread-protection measures as one quote.
Quality assurance & delivery terms
Full batch traceability from raw material to finished product. Every shipment leaves with documented inspection results, so what you approve in sampling is what arrives in production.
Certifications
- ISO 9001:2015
- RoHS
- REACH
Documents with every order
- Mill Test Certificate (MTC)
- Dimensional Report
- Salt Spray Test Report
Typical lead times
- Standard samples: 3-5 Days
- Bulk standard parts: 15-25 Days
- Custom OEM parts: 30-45 Days
Manufacturing base
- 5000 m² facility, 8 production lines
- 50-100 employees
- Monthly output 80-120 Tons
Request a Quote
Get factory-direct pricing from the manufacturer.
What to include in your Weld Fasteners inquiry
- ✓ Identify weld nut/stud type and standard, thread size and projection geometry.
- ✓ Give parent-sheet material and thickness, plus the mating component and access constraints.
- ✓ State the welding process, electrode/material compatibility and any specified weld procedure or test.
- ✓ Specify post-weld coating, corrosion protection, quantity and inspection requirements.
- ✓ Factory-direct pricing for your Weld Fasteners
- ✓ Standard and custom specifications
- ✓ Factory-direct export to buyers in Europe, Asia, the Americas and the Middle East
- ✓ Full fastener family support