
Zinc Electroplating
Zinc electroplate for steel fasteners — the workhorse finish at roughly twice the cost of phosphate & oil, 72–384 hours neutral salt spray depending on specification, with post-plate baking for hardened parts to manage hydrogen embrittlement.
Last updated: 2026-11
Specifications
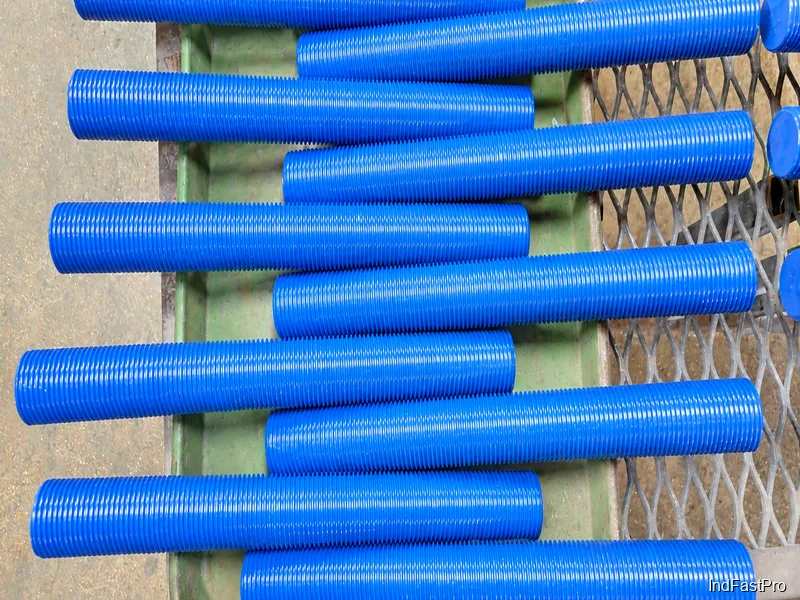
Zinc electroplate is the default corrosion finish on steel fasteners: metallic zinc deposited from a water solution by electric current. The base deposit is gray; chromate passivates make it clear, yellow, or other colors, and thickness classes trade cost for corrosion life — thinner deposits for dry indoor service, thicker for wet or saline exposure. Most fastener zinc callouts are ASTM B633 (the most common single callout in one plating shop's reported mix being Type II SC2 with yellow dichromate — the 8 µm moderate-thickness class). It is an electroplating process, so hardened high-strength parts carry hydrogen-embrittlement risk and are baked after plating; plating specifications spell out the bake procedures, which can run 24 hours or more depending on thickness.
| Process | Electroplating — cathodic deposition of zinc from ionic solution |
|---|---|
| Reference standards | ASTM B633 (fastener zinc plate) and ASTM F1941 (threaded fastener electroplate); baking per ASTM B850 |
| Common callout | ASTM B633 Type II SC2, yellow dichromate — SC2 is the moderate 8 µm (0.0003″) thickness class |
| Corrosion resistance | 72–384 h neutral salt spray by specification — e.g. B633 Type II SC2: 96 h; F1941 FE/ZN 8C: 120 h; GMW3044 clear variants: 72 h and 240 h; Ford S437: 384 h with COF 0.15 |
| Appearance | Gray deposit; clear or yellow (and other colors) via chromate/passivate |
| Lubricity | Moderately rough surface, lower lubricity than plain steel; sealers and lubricant topcoats improve friction and corrosion performance |
| Hydrogen embrittlement | Electroplated process — hydrogen risk for hardened high-strength parts; post-plate bake required, up to 24 h+ by thickness (parts above ~39 HRC baked per shop practice) |
| Relative cost | About twice phosphate & oil (reported plating-shop comparison) |
Materials
- Carbon steel fasteners
- Alloy steel fasteners (baked after plating)
- Case-hardened fasteners (baked after plating)
Ordering & documentation
Documents
Shipments are backed by Mill Test Certificate (MTC), Dimensional Report, Salt Spray Test Report on request, with full batch traceability from raw material to finished product. Quality management follows the owner-confirmed compliance list: ISO 9001:2015, RoHS, REACH. Exact document sets are confirmed on the order.
Quotation
- The fastener family (Zinc Electroplating) plus the standard designation from your drawing — DIN / ISO / JIS / ASTM / ANSI, or a drawing for custom parts.
- Size (diameter and length), thread type (metric or inch), property class or grade, and coating or finish.
- Quantity per size and your target delivery date.
- Destination country, and any required documents (for example a mill test certificate) so the quote includes them.
Sample & supply
Minimum order quantity is per batch, carried with the fastener order. Finishing run adds 5–10 days to the fastener lead time. Quantities or variants outside the standard range are confirmed at quotation.
Storage & shipping
Parts are packed for export and shipped factory-direct to buyers in Europe, Asia, the Americas and the Middle East. Store fasteners dry and protected until installation, and keep coated parts in their packaging until use; specific packing and preservation requirements can be stated on the order and confirmed at quotation.
Frequently asked questions
When is zinc electroplate the right finish?
For the broad middle of fastener work: indoor and sheltered service, painted assemblies, and outdoor parts whose spec accepts the 72–240 hour salt-spray class of a standard thickness. It costs about twice phosphate & oil but adds real corrosion life, and unlike zinc flake or zinc-nickel it is available everywhere at short lead. Move up when the spec demands more hours than a standard zinc class delivers, or when hardened high-strength parts make the bake requirement unwelcome — that is zinc flake territory.
What is the MOQ and lead time for this finish?
Finishing runs per batch carried with the fastener order and adds 5–10 days to the fastener lead time. Coated parts follow the finish line that processes them, so confirm the exact schedule against quantity and finish class at quotation.
What should an RFQ for this finish state?
State the base fastener (grade, diameter, length), the coating standard and class (or the process plus thickness/color requirement where no standard callout exists), any salt-spray or friction requirement, and quantity per size — plus destination country and required documents such as a mill test certificate.
Related knowledge
- Reading a Fastener Coating Callout: ISO 10683 Designations, Salt-Spray Hours and What to Confirm With the Plater
- Zinc-Plated vs Hot-Dip Galvanized Fasteners: Which Coating for Which Environment
- Zinc-Flake Coating for Fasteners: When the Evidence Supports It, and What to Verify at the Coater
- Zinc-Flake vs Zinc-Nickel for High-Strength Fasteners: What the Evidence Settles on Hydrogen, Salt Spray, Friction and Specs
Request a Quote
Get factory-direct pricing from the manufacturer.
What to include in your inquiry
- ✓ Standard and property class (e.g. DIN 912, ISO 4762, class 8.8) — or a drawing for custom parts.
- ✓ Sizes, lengths and thread type (metric or inch).
- ✓ Quantity per size and your target delivery date.
- ✓ Destination country, plus any coating or finish requirement.
- ✓ Any documents you need with the shipment (e.g. mill test certificate) so the quote includes them.
- ✓ Your inquiry goes straight to the factory team by email and gets a reply within 24 hours.
- ✓ Factory-direct pricing
- ✓ Standard and custom specifications
- ✓ Factory-direct export to buyers in Europe, Asia, the Americas and the Middle East
- ✓ Full fastener family support